TL;DR & Quick Summary
A return visit because the technician didn't have the part costs a second truck roll, another slot in the schedule, and a less happy customer. Most field service companies respond by adding more parts to every van. That fills the shelves, ties up capital and still leaves gaps, because first-time fix depends on having every part a job needs, not most of them.
Measure job-level hit rate, not part availability. Three parts at 95% each gives about 86% of jobs fully covered
Stock slow parts with Poisson probabilities, not averages and gut feel
Rank by value per shelf space: van space, not money, is usually the binding limit
Differentiate vans by territory, equipment base and technician specialism
Predict parts per job from booking data, which often beats any change to the general stock list
Key Takeaway: The best stock list comes from data about which missing parts cause return visits. The fastest improvement usually comes from predicting the specific job's parts before the van leaves.
Get Started: Want to see which parts are causing your repeat visits? Schedule a strategy call with Cogniq AI or explore our predictive analytics services.
Why "Carry More" Doesn't Fix First-Time Fix
Consider how first-time fix actually works. A job is completed on the first visit only if all the parts it needs are on the van. If parts are available independently, job coverage is the product of their individual availabilities:
| Parts needed per job | Each part at 95% | Each part at 98% |
|---|---|---|
| 1 | 95% | 98% |
| 2 | 90% | 96% |
| 3 | 86% | 94% |
| 5 | 77% | 90% |
This explains a common frustration. The inventory report says 95% part availability, yet a meaningful share of multi-part jobs still need a return visit. Raising every part a little is expensive and gives limited gains. The better approach is to find the specific parts that most often cause return visits and to predict job-specific parts before dispatch.
So the first metric to track isn't part availability. It's van hit rate: the share of jobs where every required part was on the vehicle. Most field service platforms record parts used per job and return visits per job. Joining those two tells you which missing parts cause second trips.
Step 1: Build the Demand Picture Per Van
Pull 6–12 months of job history, and at least a full year if your work is seasonal, with:
- Parts used per job, including quantity
- Which van and technician did the job
- Job type, equipment make and model where recorded
- Whether a return visit was needed, and which part was missing
Calculate each part's usage per replenishment cycle per van. If vans restock weekly, the question is: how many of this part does this van use in a typical week?
You'll find that most parts are intermittent. They're used in some weeks and not in most. That changes how they should be forecast and stocked. Methods designed for sparse demand, such as SBA and TSB, are covered in our guide to intermittent demand forecasting. Averages alone mislead here.
Step 2: Stock Slow Parts With Probabilities
For parts used a few times per cycle or less, the Poisson distribution gives a good first model of usage. Take a part used on average 0.5 times per weekly cycle:
| Units carried | Probability of covering the week's demand |
|---|---|
| 0 | 61% |
| 1 | 91% |
| 2 | 99% |
| 3 | 99.8% |
The first unit covers most of the need. The second closes most of the remaining gap. The third adds almost nothing. That pattern, with large gains from the first unit and fast-falling gains after it, is typical for slow parts, and it's why a standard "carry two of everything" rule wastes space.
To decide whether each extra unit is worth carrying, compare:
- The expected cost it prevents: the probability that demand reaches that unit, multiplied by the cost of a missed part (the second visit, the delay and any SLA penalty)
- What it costs to carry: the capital tied up, the risk of damage or obsolescence, and, most importantly, the shelf space it uses
For the example part, the probability that demand reaches the second unit is about 9%, and the third about 1.4%. If a second visit costs a few hundred in labour and travel, the second unit is usually justified. The third usually isn't, unless the part is critical or very small.
For faster-moving consumables such as fittings, filters and fuses, a standard safety stock approach works better. See safety stock calculation formulas.
Step 3: Rank by Value Per Unit of Space
In most fleets the binding constraint isn't money. It's shelf space. A van can only hold so much, and a bulky part that is rarely used can displace several small parts that are used often.
A practical ranking approach:
- For every part and quantity, calculate the expected cost avoided by carrying that unit (Step 2)
- Divide by the space the unit takes, by shelf slot, bin size or volume
- Sort all part-units by that ratio, highest first
- Fill the van down the list until space runs out
This treats every unit, not every part, as a separate decision. The first capacitor can rank far above the second compressor contactor even when the contactor matters more per unit. The approach is simple enough to run in a spreadsheet, and it makes the trade-offs visible to service managers.
Two adjustments keep it realistic:
- Critical-part overrides: parts required for safety or emergency work, or needed under contractual response times, go on the van regardless of the ranking
- Kits: parts almost always used together should be ranked and stocked as a kit, since carrying one without the other gives little benefit
Step 4: Different Vans, Different Lists
A single standard list for every vehicle is easy to manage, but it's rarely right. Demand differs by:
- Territory: housing age, commercial versus residential mix, and which equipment brands are common locally
- Technician specialism: installation vans and repair vans use very different parts
- Contracts: a service agreement for a specific equipment fleet can justify dedicated stock on the vans that serve it
- Season: HVAC vans in particular need different stock between heating and cooling seasons
A workable compromise is a core list shared by all vans plus a variable section calculated per van or per territory. The core list keeps operations simple. The variable section is where the data-driven gains are.
Step 5: The Warehouse Behind the Van
The van is the last level of a supply chain: central warehouse, branch or depot, then the vehicle. How much a van needs to carry depends on how fast it can get a part from the level above. If a branch can deliver within hours, or a technician can collect on the way to the next job, the van can carry less of the expensive, slow parts.
Setting stock levels across all these levels together, rather than separately, has a long history in operations research, going back to Sherbrooke's METRIC model (1968) for military spare parts. You don't need a full multi-level model to use the principle. When deciding van stock, account for how quickly and cheaply the part can be obtained from the depot.
Step 6: Predict the Job's Parts Before Dispatch
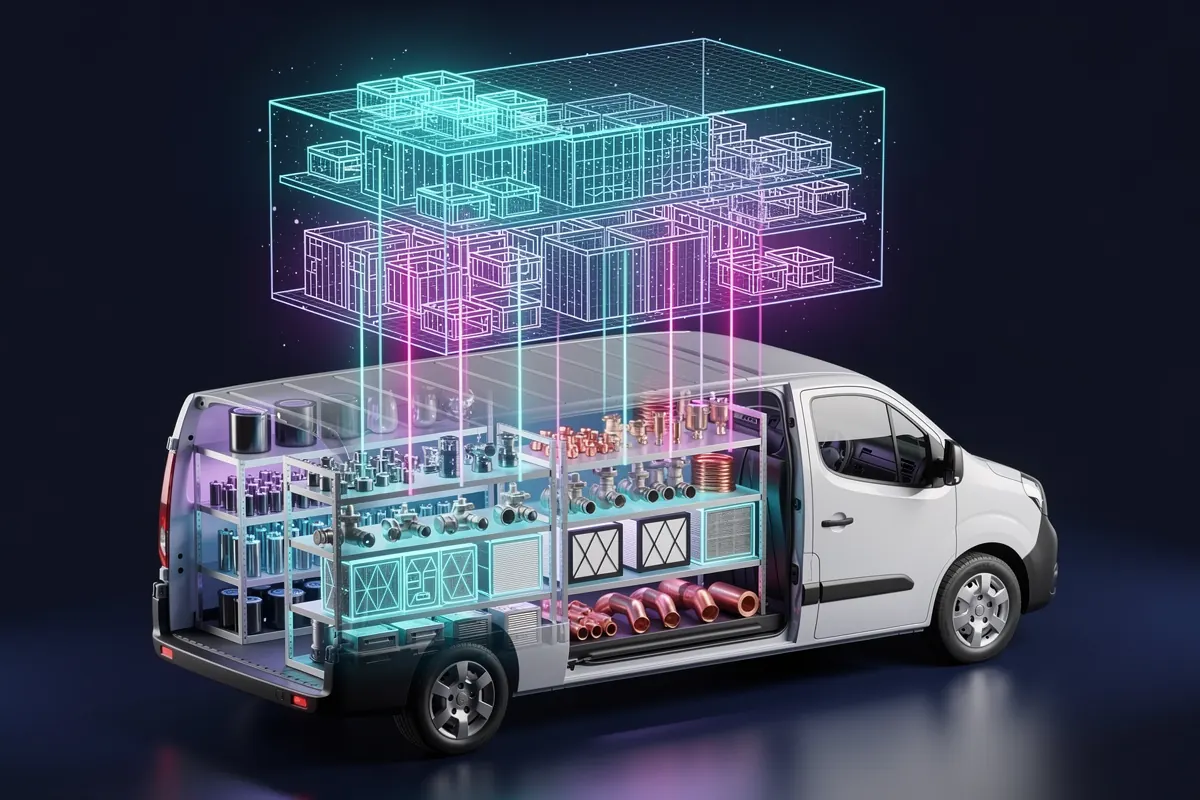
This is where the largest improvements in first-time fix usually come from. Much of the information needed to predict a job's parts is available when the job is booked:
- Equipment make, model and age, from the customer record or asked at booking
- The reported symptom, for example "no cooling", "leaking" or "error code E4"
- Service history for that customer and unit
- What parts were used on similar past jobs for the same equipment and symptom
A model trained on past jobs can turn this into a likely-parts list for each booking. The dispatcher or technician can check it against van stock before leaving, and pick anything missing from the depot. The model doesn't need to be perfect. It needs to flag the parts most likely to be missing often enough to prevent a meaningful share of return visits.
The quality of this prediction depends on the booking data. A customer service agent or AI receptionist that reliably captures equipment model and symptom at intake makes parts prediction far more accurate. That link between intake and dispatch is part of the wider automation described in our guide to AI field service automation. Connecting booking, job history and inventory data is usually the real engineering work, which is what our AI integrations practice handles.
Step 7: Keep the List Alive
Truck stock lists go stale quickly. Build these reviews in:
- Monthly or quarterly recalculation of quantities from recent job data
- Removal flags for parts with no usage over several cycles. Forecasting methods such as TSB let the forecast fall as demand stops, which is useful for parts tied to ageing equipment
- Structural review when equipment models, contracts, territories or seasons change
- Shrinkage checks: compare what the system says is on the van with regular counts. A stock list is only useful if the van actually contains it
A Realistic Starting Point
You don't need a large project to start. A useful first step is:
- Join job history to parts used and return visits
- List the parts that most often caused a return visit in the last year
- Calculate Poisson-based quantities for those parts per van
- Check whether they fit in the space currently used by parts that are rarely used
That analysis often shows quick wins in a few weeks. Parts prediction at booking is the second step. It needs more integration work, and it's where the larger gains usually are.
Conclusion
Truck stock optimization is a probability problem with a space constraint. Measure job-level hit rate, not part availability. Stock slow parts with probabilities rather than rules of thumb. Rank units by value per unit of space. Tailor lists to each van's real work. Then add prediction at booking so each van carries the right parts for its next job, not just the common ones.
Schedule a strategy call with Cogniq AI to analyse which parts are driving your return visits, or explore our predictive analytics services.